What Are the Benefits of Working With Chemical Wholesalers for Regular Bulk Orders?
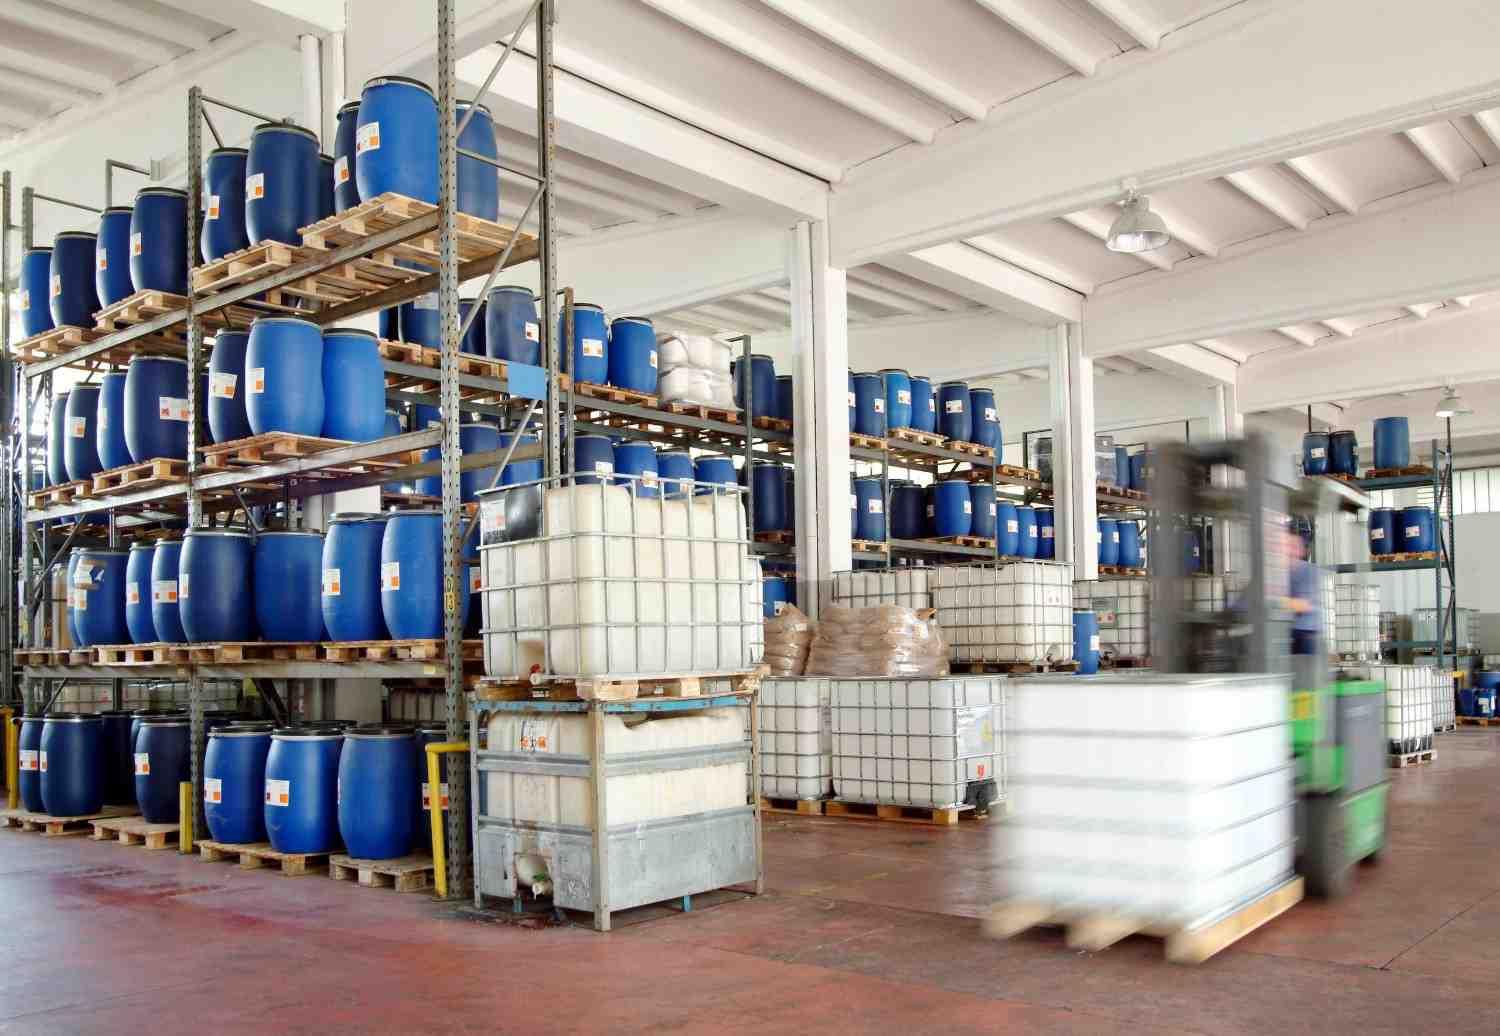
I used to think buying industrial chemicals was mostly about tracking down a supplier, checking the price, and then getting delivery sorted. It sounded simple enough, really, like… done. But once I started digging into how businesses actually source chemicals for regular production, I figured out there are quite a few factors that can trip you up, or at least slow everything down. Things like product availability, packaging, storage , and safe handling can all impact whether a job runs smoothly or turns into that long “why is this not here yet” kind of week.
My curiosity really kicked in when I was trying to understand how manufacturers keep their operations going without constantly chasing down material shortages. That’s when I started looking into how Chemical Wholesalers support businesses that depend on a steady supply of chemical products, not just a random buy whenever.
Why did I start looking into chemical wholesalers?
Honestly, the main reason was to understand what happens in the middle, between a chemical manufacturer and the business that actually uses the product. Picture a workshop, or a factory, that needs certain chemicals every week, on a schedule that can’t really be moved. If a delivery shows up late, or the material arrives in unsuitable packaging, even a small issue can mess up the day , sometimes more than people expect.
During my research into industrial suppliers I came across Chemical Solutions while I was reading about chemical processing services. It kinda made me rethink it , because some businesses don’t just need a simple purchase. They might need processing, repackaging, or a bit of preparation first, before the chemical is ready to be used the way they need.
I also noticed that different industries come with different expectations too. One business might want liquid inputs in containers that are practical to handle, while another might require dry powders in exact amounts. Having a supplier that understands those little differences can make ordering feel less tangled and more like a path you can actually follow.
How do chemical wholesalers support industrial businesses?
That’s one of the questions I wanted answered, because “wholesaler” sounds broad. In general, wholesalers help businesses source chemical products in quantities that match how their operations run. Depending on the service level, they may also coordinate things like packaging arrangements, storage needs, and other supply requirements.
Some businesses need extra processing before the materials can be put to work. Services like powder blending, chemical sieving and filtering, plus chemical crushing and packing can be important when a product has to match specific applications. Liquid and powder packing can matter too, especially when suppliers have to provide different package sizes for different workflows.
What I found kind of interesting is that these services do not always show up with every supplier. Some focus mostly on distribution, and that’s it, while others go further by using suitable facilities , or relying on specialist partners to handle the extra steps.
If you’re looking at chemical toll manufacturing Australia options, that difference becomes pretty important. The best setup depends on the product itself, production volume, what equipment you have, and how much processing is actually needed before the material is usable.
What did I notice about the process?
One thing that stood out was how much planning tends to happen before a chemical order is even dispatched. Product specs need to be clear, quantities must be correct, and packaging has to match the material. It sounds obvious, but those details can be easy to overlook when someone is focused only on the price, and not on the “how will this behave in the real world” part.
Chemical repacking is another example. Transferring material into different package sizes requires appropriate procedures and equipment. Where regulated substances are involved, dangerous goods handling and relevant transport requirements also need careful attention.
I also figured out that chemical storage solutions can be a key part of the broader supply process. Some substances really do need specific storage setups, separation, or little extra controls, otherwise safety and product integrity can get compromised, pretty fast.
For manufacturers, services like contract chemical manufacturing and paste and putty manufacturing might be relevant too, especially if production needs specialist equipment or extra prep work. What’s actually on offer, will depend on the provider, and sometimes that part is easy to assume but not always accurate.
What Are the Actual Benefits of Working With a Reliable Supplier?
From what I gathered, the big win is usually a more organised approach to sourcing materials. When supply arrangements are reliable, businesses can plan stock levels, align production timings, and reduce the odds of surprise shortages showing up at the worst moment.
Working with someone who’s experienced can also make it easier to talk through packaging options, delivery quantities, and the technical expectations before any order is placed. That’s particularly handy for companies managing several products, or when production volumes drift across the year.
Still, picking a supplier is not a “set it and forget it” situation. I would check product availability, the paperwork, delivery logistics, storage practices, and how familiar they are with the specific chemicals involved. Clear communication matters just as much. You do not want to realise there’s a packaging issue, after the delivery is already sat there.
Final Thoughts
Digging into the industrial supply process gave me a better feel for how much effort sits behind keeping manufacturing going. It’s not just buying chemicals and then waiting for a truck to arrive. Ongoing supply, suitable packaging, careful handling, and straightforward communication all play their little roles, even if it’s easy to overlook.
For businesses comparing Chemical Wholesalers, I’d look past the price tag and ask whether the supplier can handle the real operational needs. When product supply and any required processing are properly coordinated, managing day-to-day production can become a little more straightforward.